
Facility
Flexible production from samples to large-scale batches with reliable Japanese-made equipment
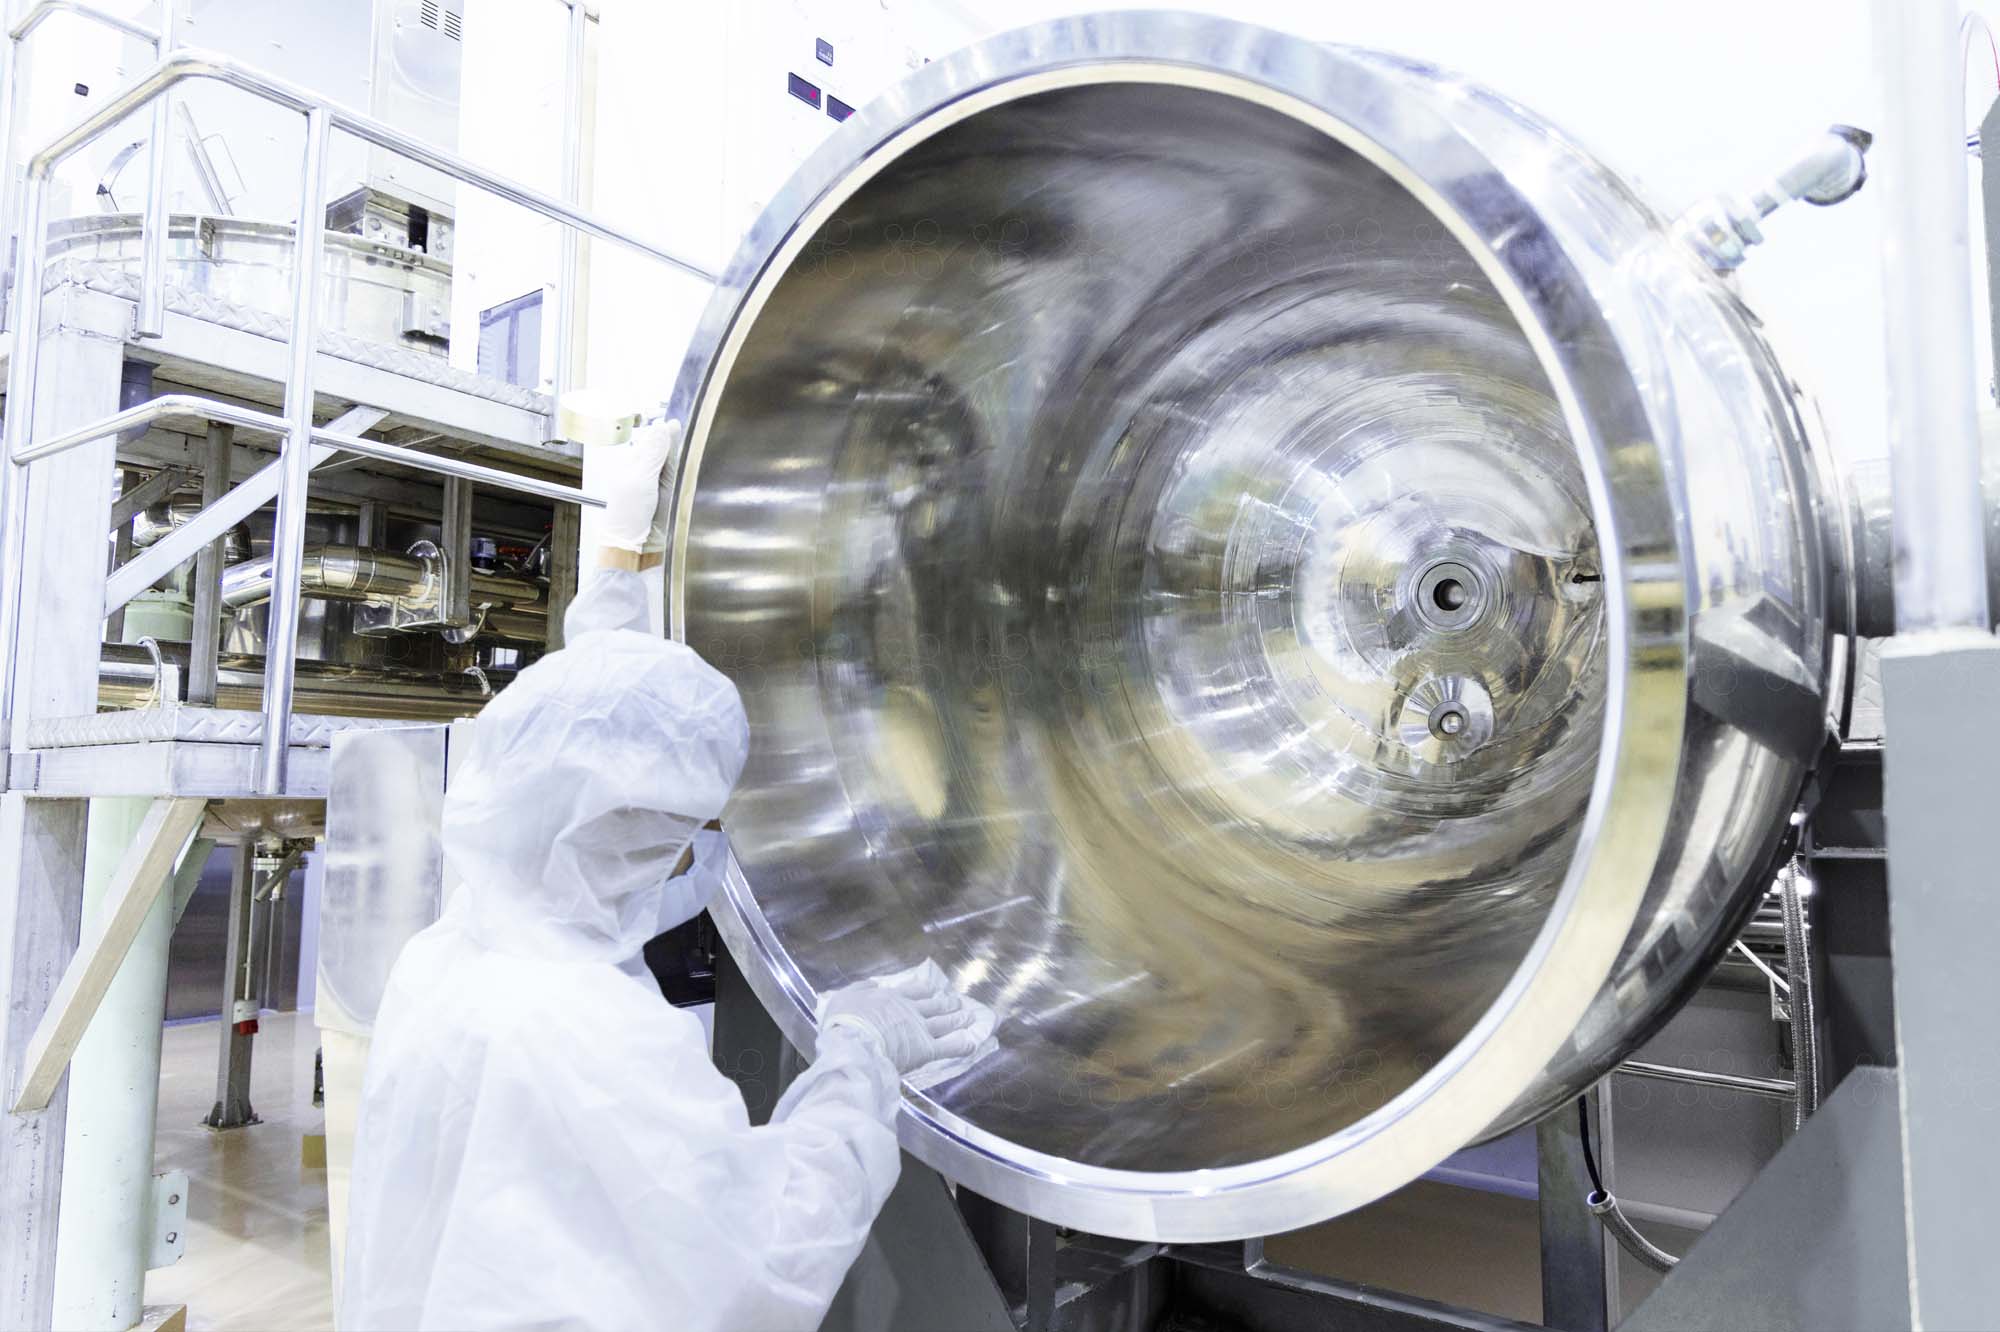
Our manufacturing facility is designed in strict compliance with cGMP, ISO 22716, and FDA standards. All production equipment is carefully selected with top priority given to quality, safety, and efficiency, sourced primarily from reputable Japanese manufacturers. In particular, our purified water system and HVAC control system – both of which directly affect cosmetic product quality – utilize advanced Japanese technology. Our diverse range of manufacturing and packaging machinery enables us to flexibly respond to various product types and production scales. With multiple mixing systems and filling machines, we are capable of handling everything from small pilot batches for product development to large-scale commercial production with efficiency and consistency.
R&D
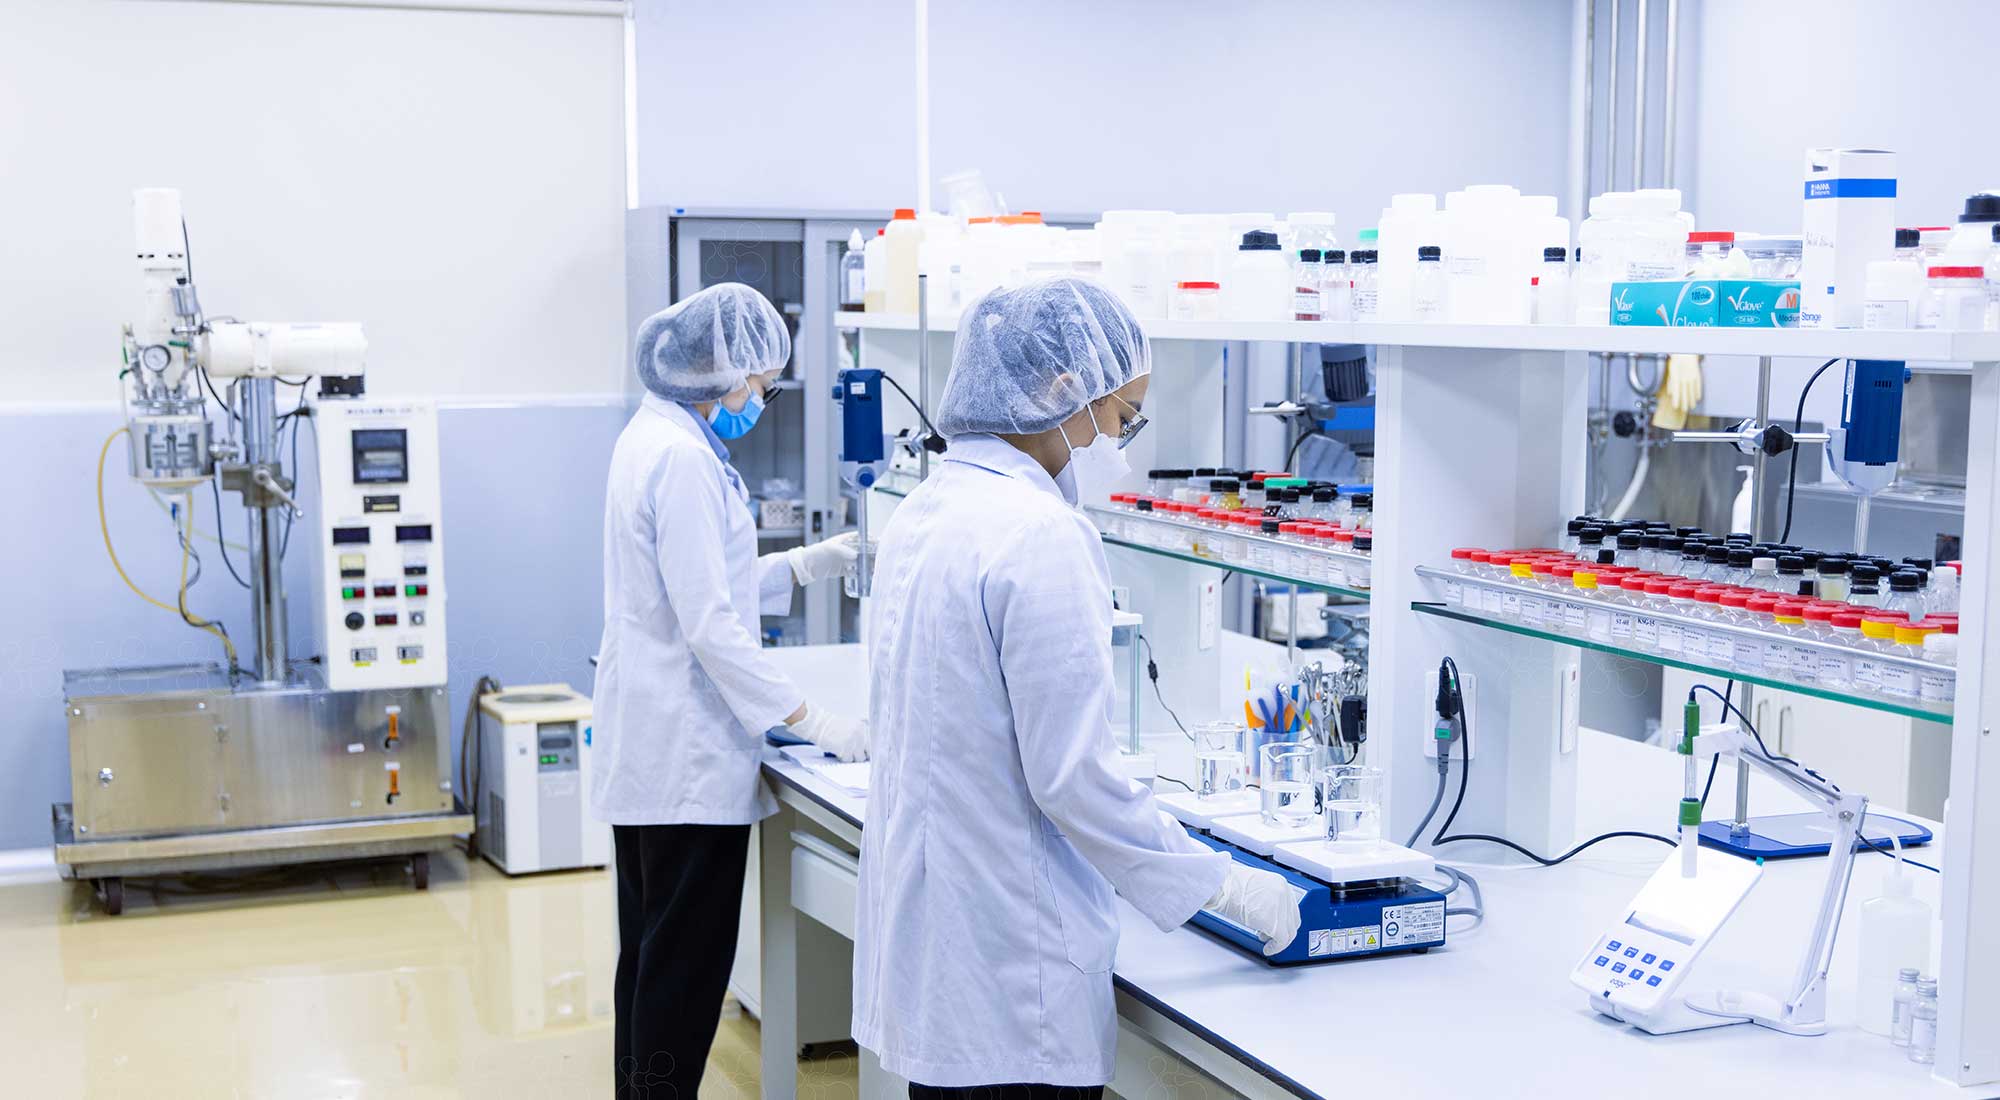
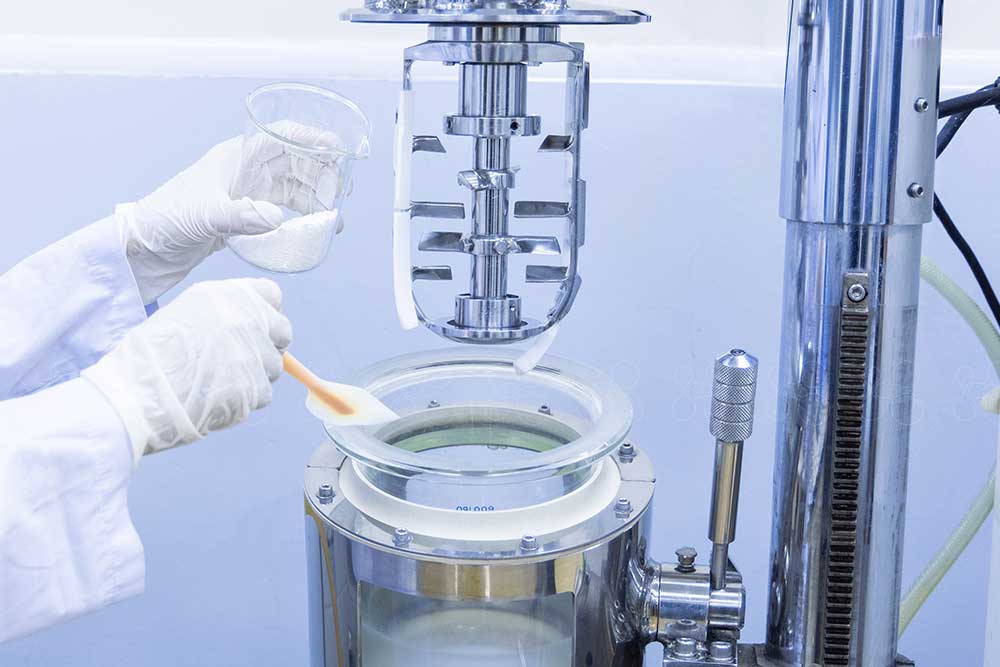 The R&D Department not only develops formulations tailored to diverse customer needs, but also proposes products based on current market trends. New ingredients are carefully evaluated for efficacy and safety before being adopted, and their features are reflected in the product concept. In formulation development, we prioritize not only performance and originality, but also safety. Before full-scale production, we conduct repeated sample creation in the lab and trials on the production line to ensure product quality and stability. We also place great importance on biodiversity and innovation in raw material sourcing. In line with our corporate vision, we strive to minimize the use of petroleum-based synthetic ingredients, and instead focus on developing products that harness the inherent power of natural-origin materials.
Quality Management
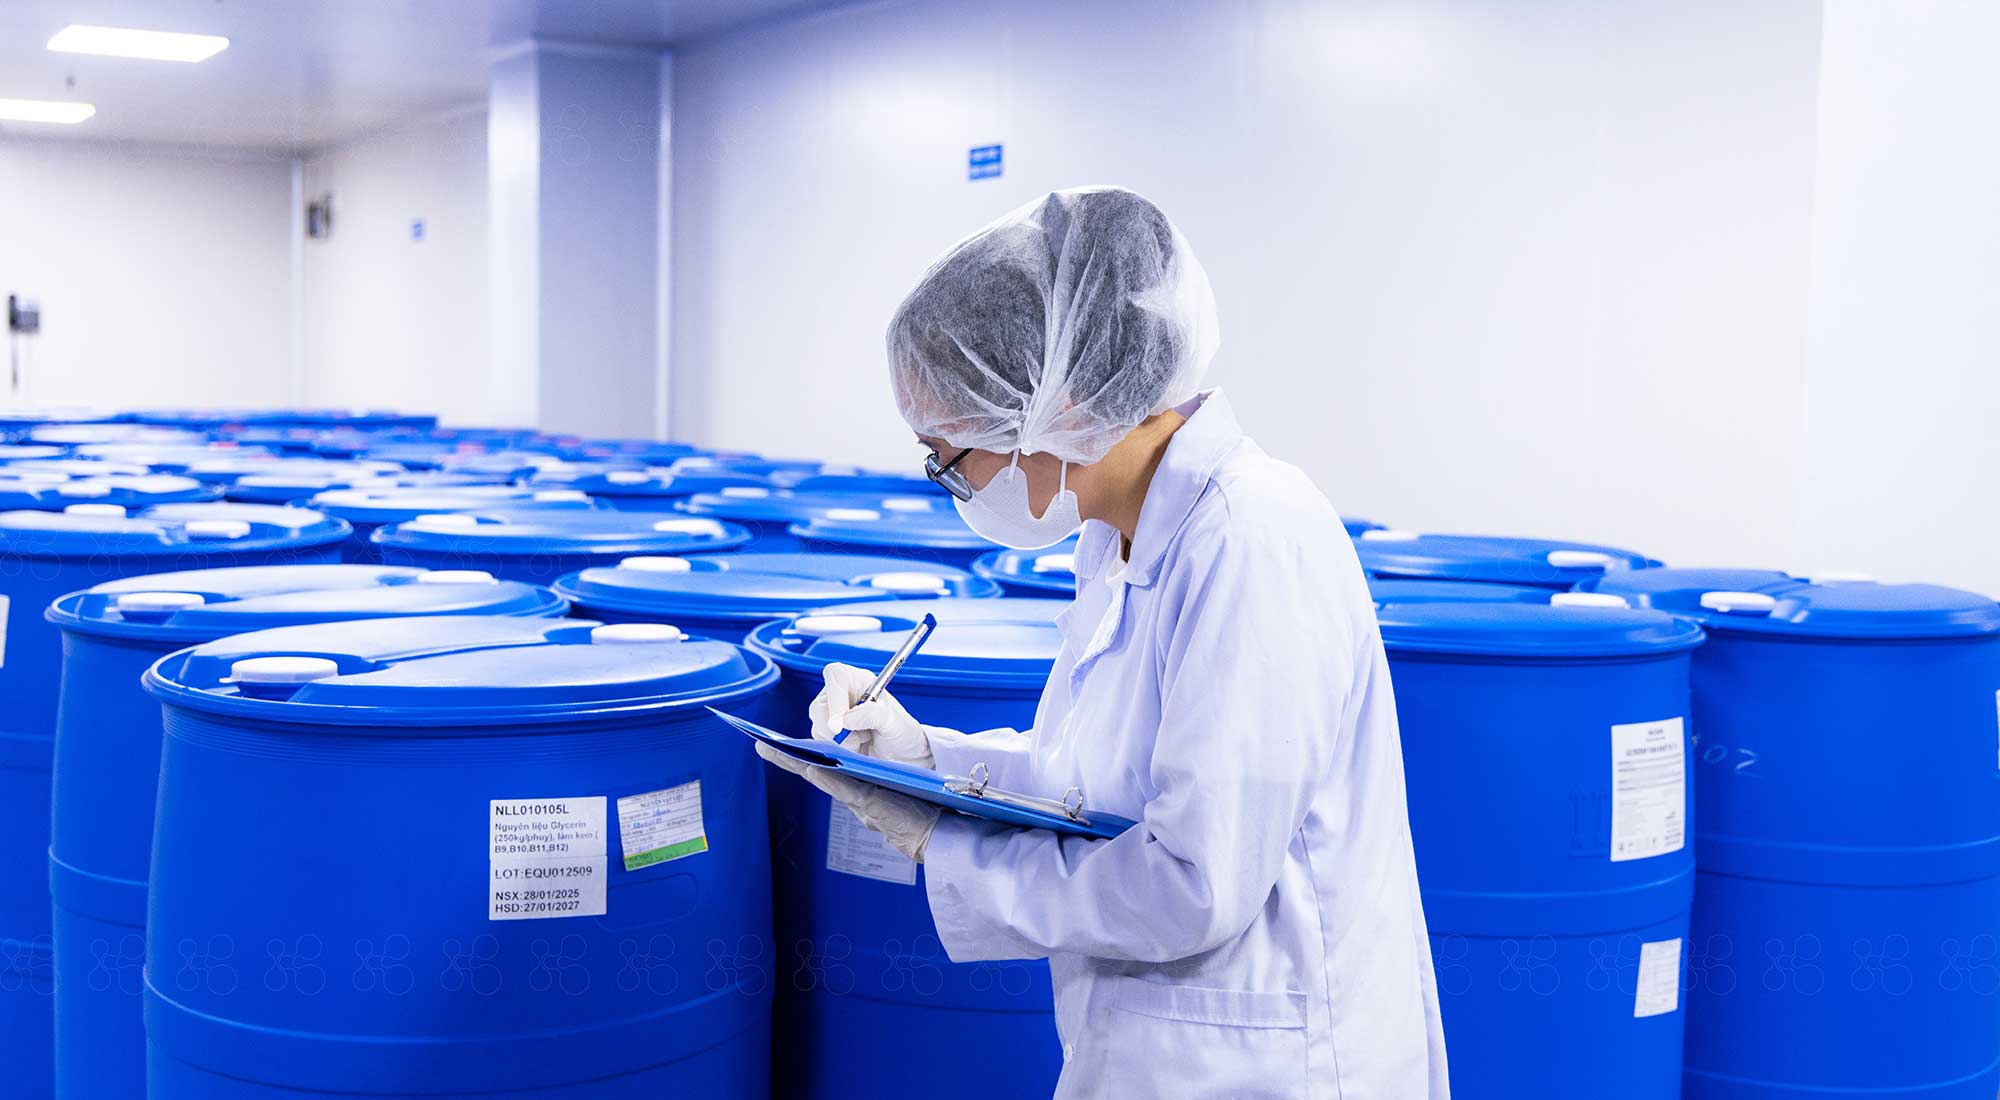
Raw materials and packaging components are subject to incoming inspections by our Quality Control Department. Only those that pass the quality checks are approved for storage. Finished products undergo a series of tests, including viscosity and pH measurements, as well as microbiological inspections. Only products that meet all established standards are approved for shipment.
Manufacturing
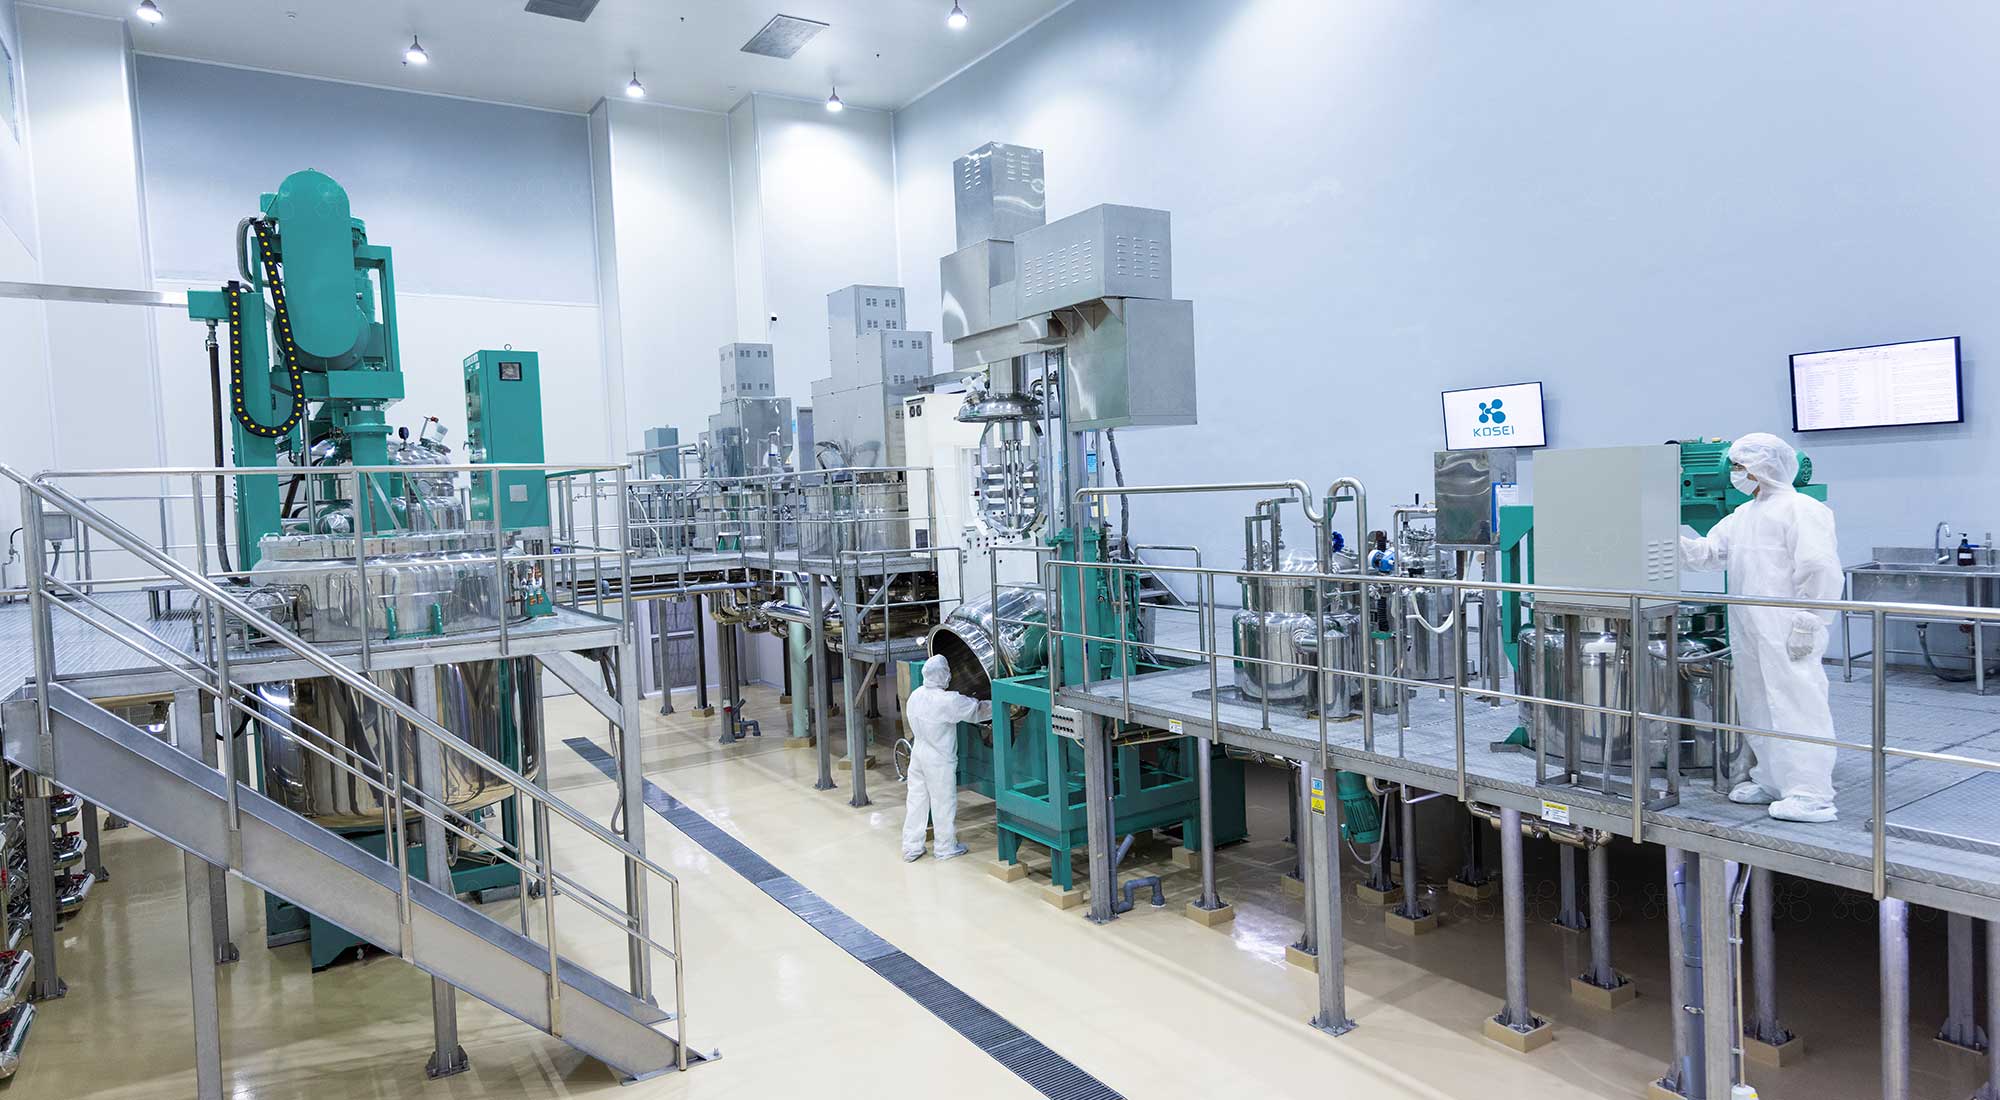
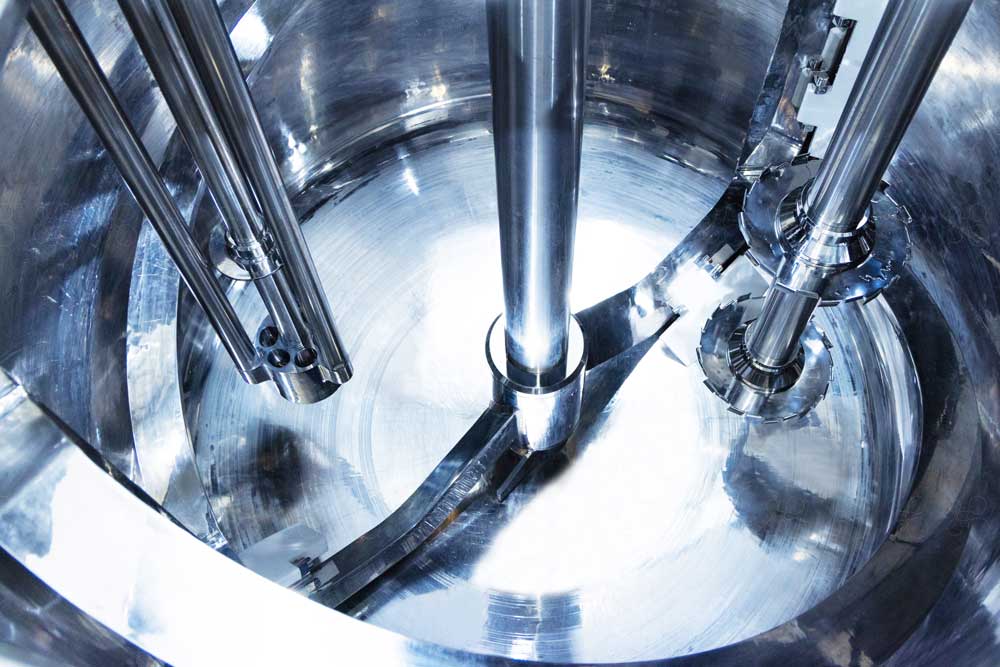 Our production processes are carried out in a clean and controlled environment in compliance with cGMP, ISO 22716, and FDA standards. We utilize a wide range of mixing equipment, including vacuum emulsifying machines, to manufacture a variety of formulations from liquids to high-viscosity creams. With mixing capacities ranging from 100 to 3,000 liters, we are able to flexibly accommodate both small-batch and large-scale production requirements.
Filling and Packaging
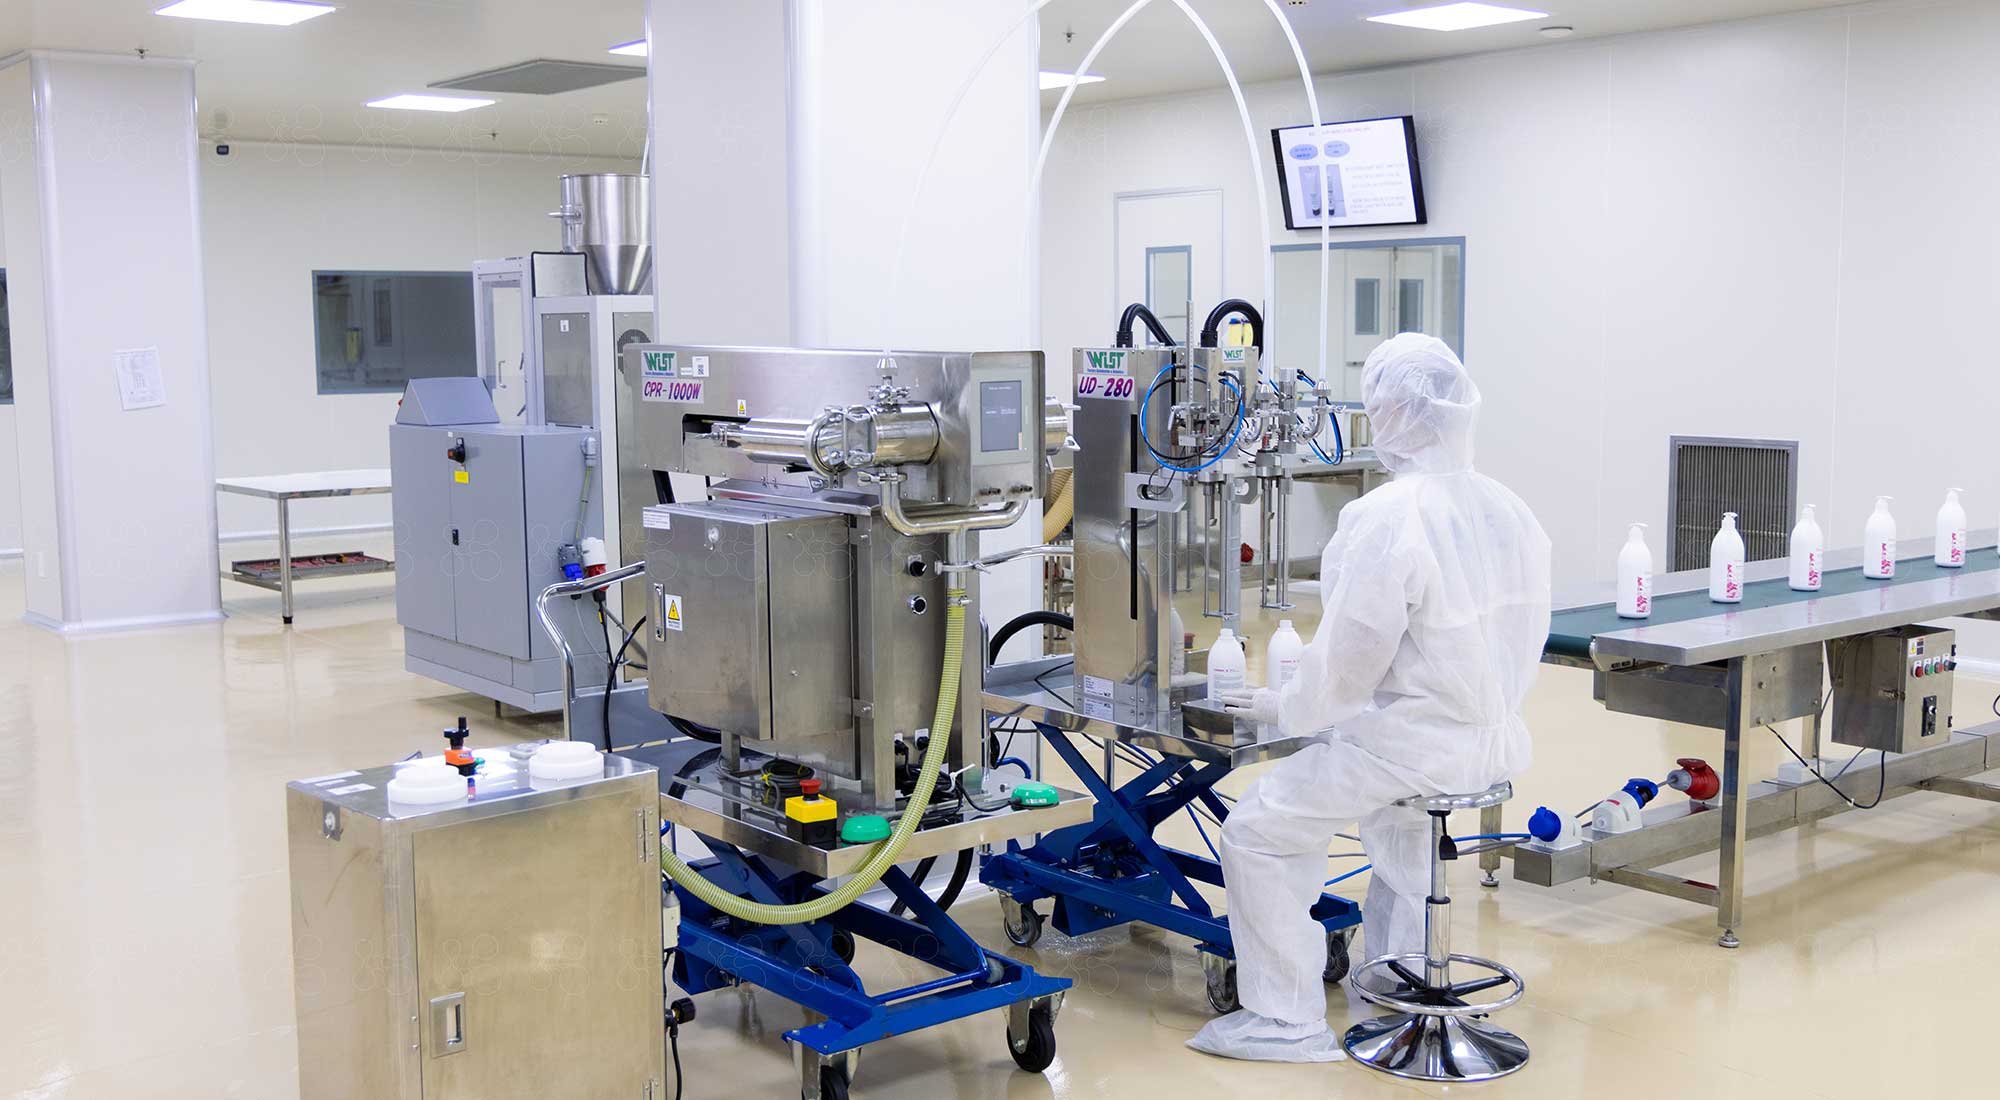
Bottle, jar, and spout pouch filling machines
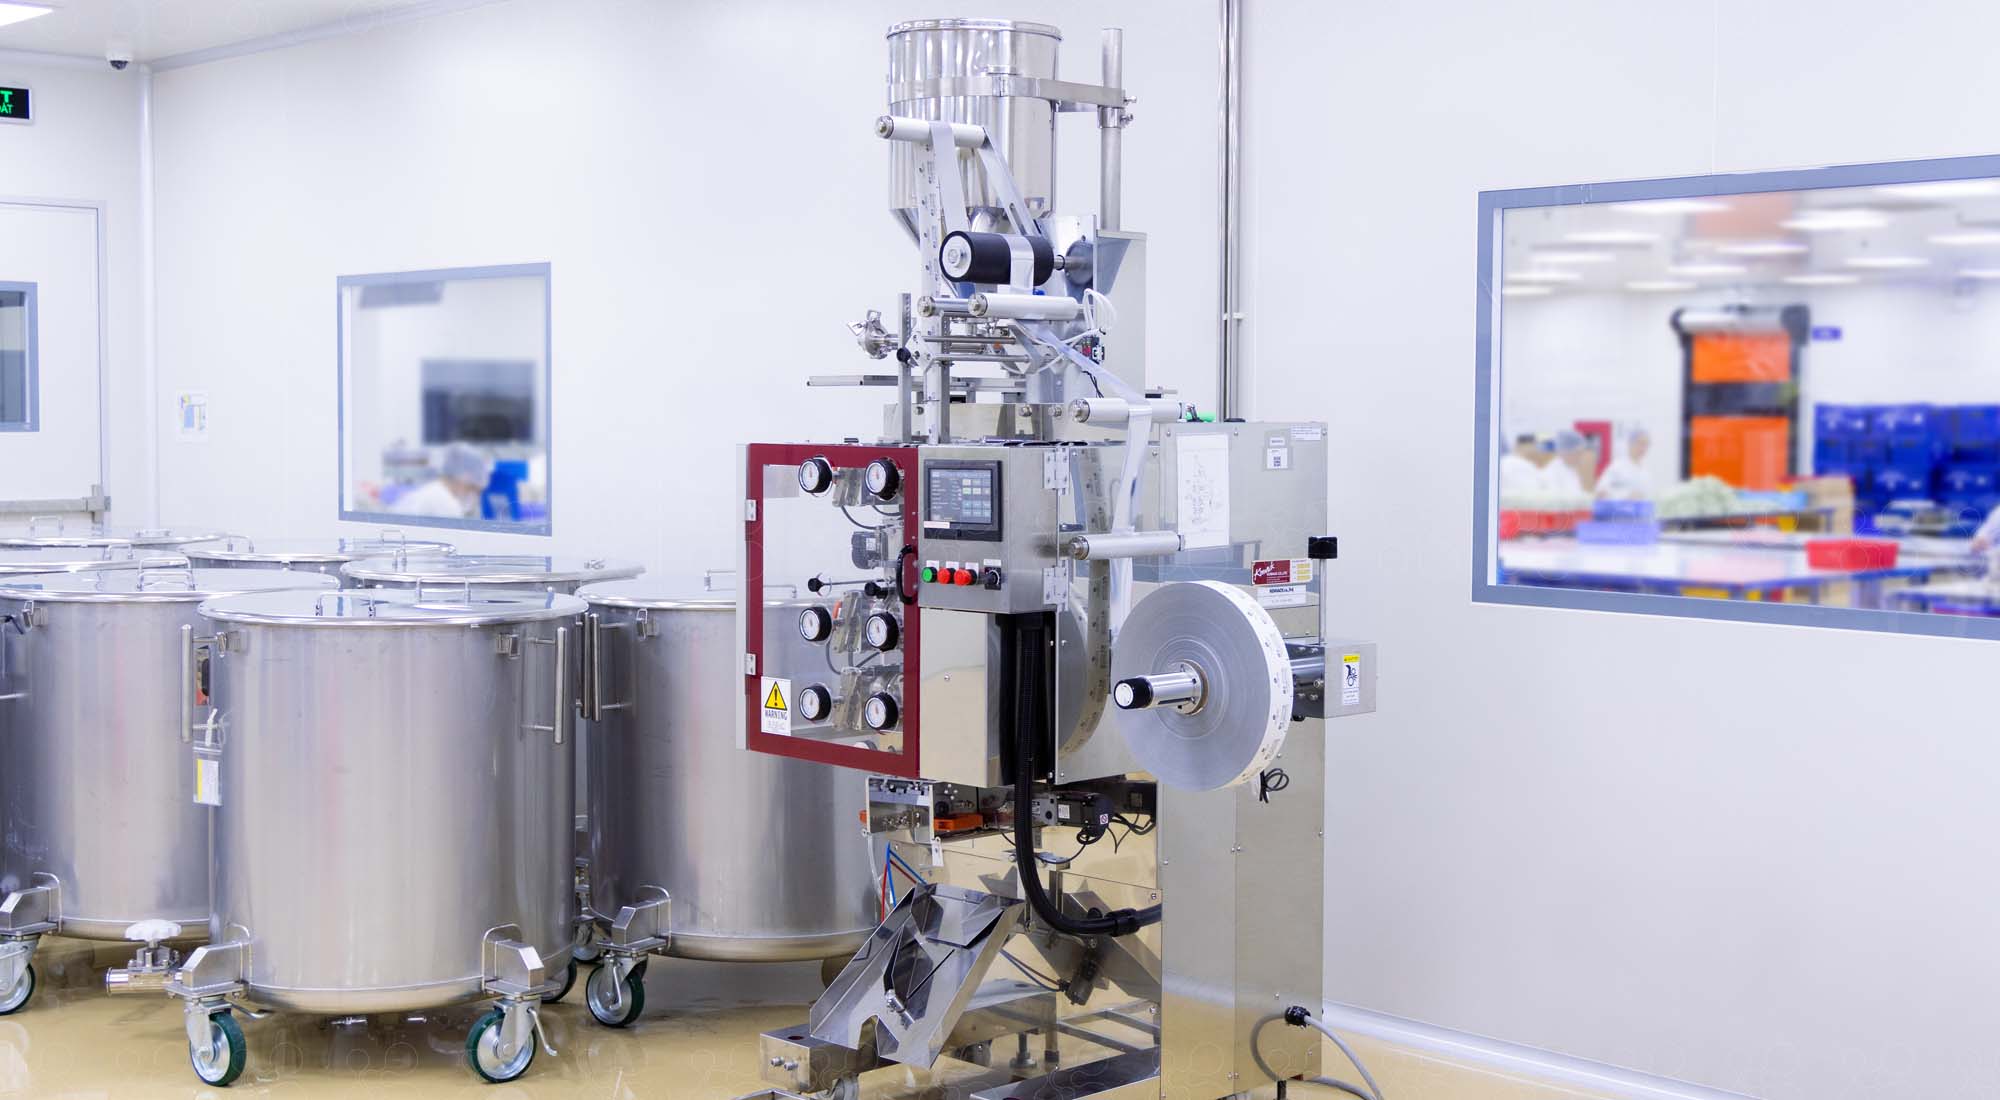
Paper pouch and plastic pouch filling machines
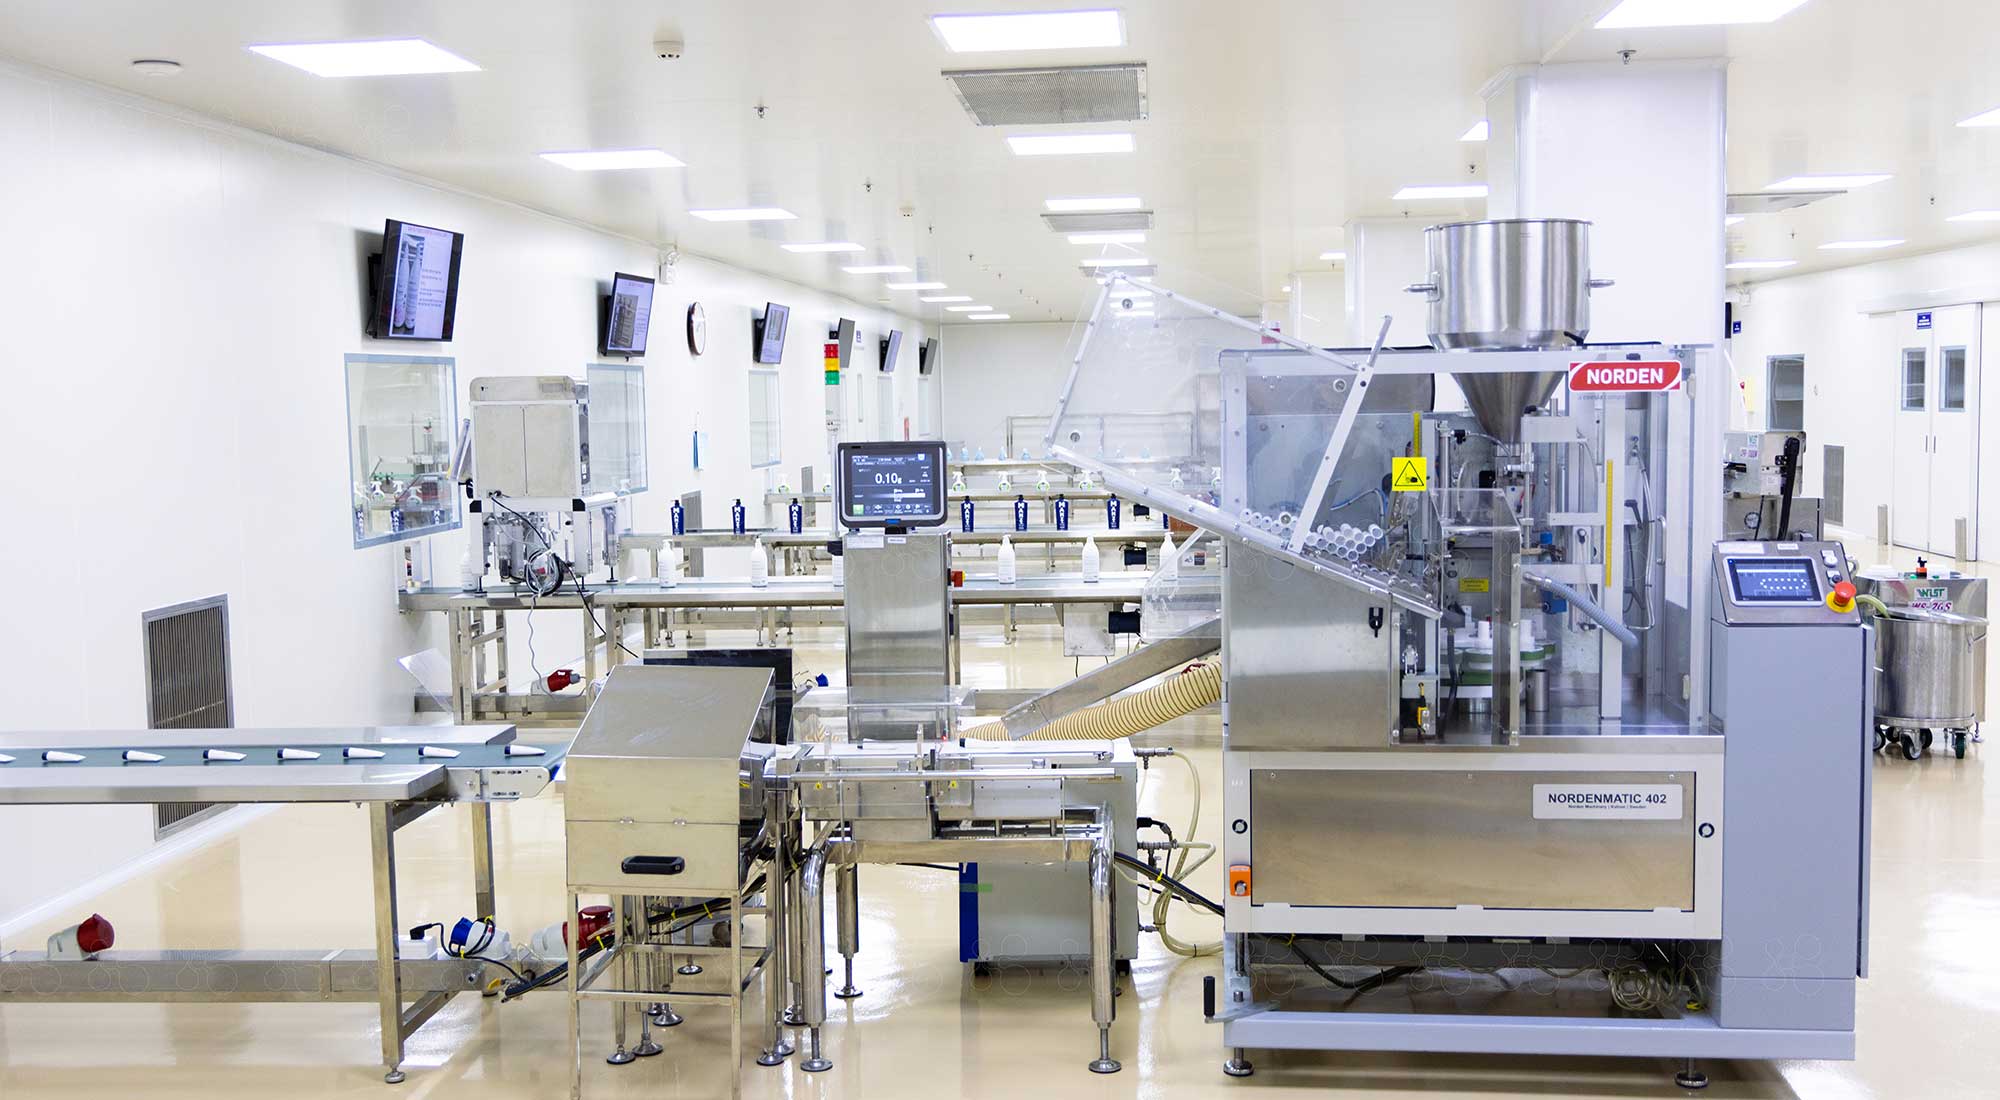
Aluminum tube and plastic tube filling machines
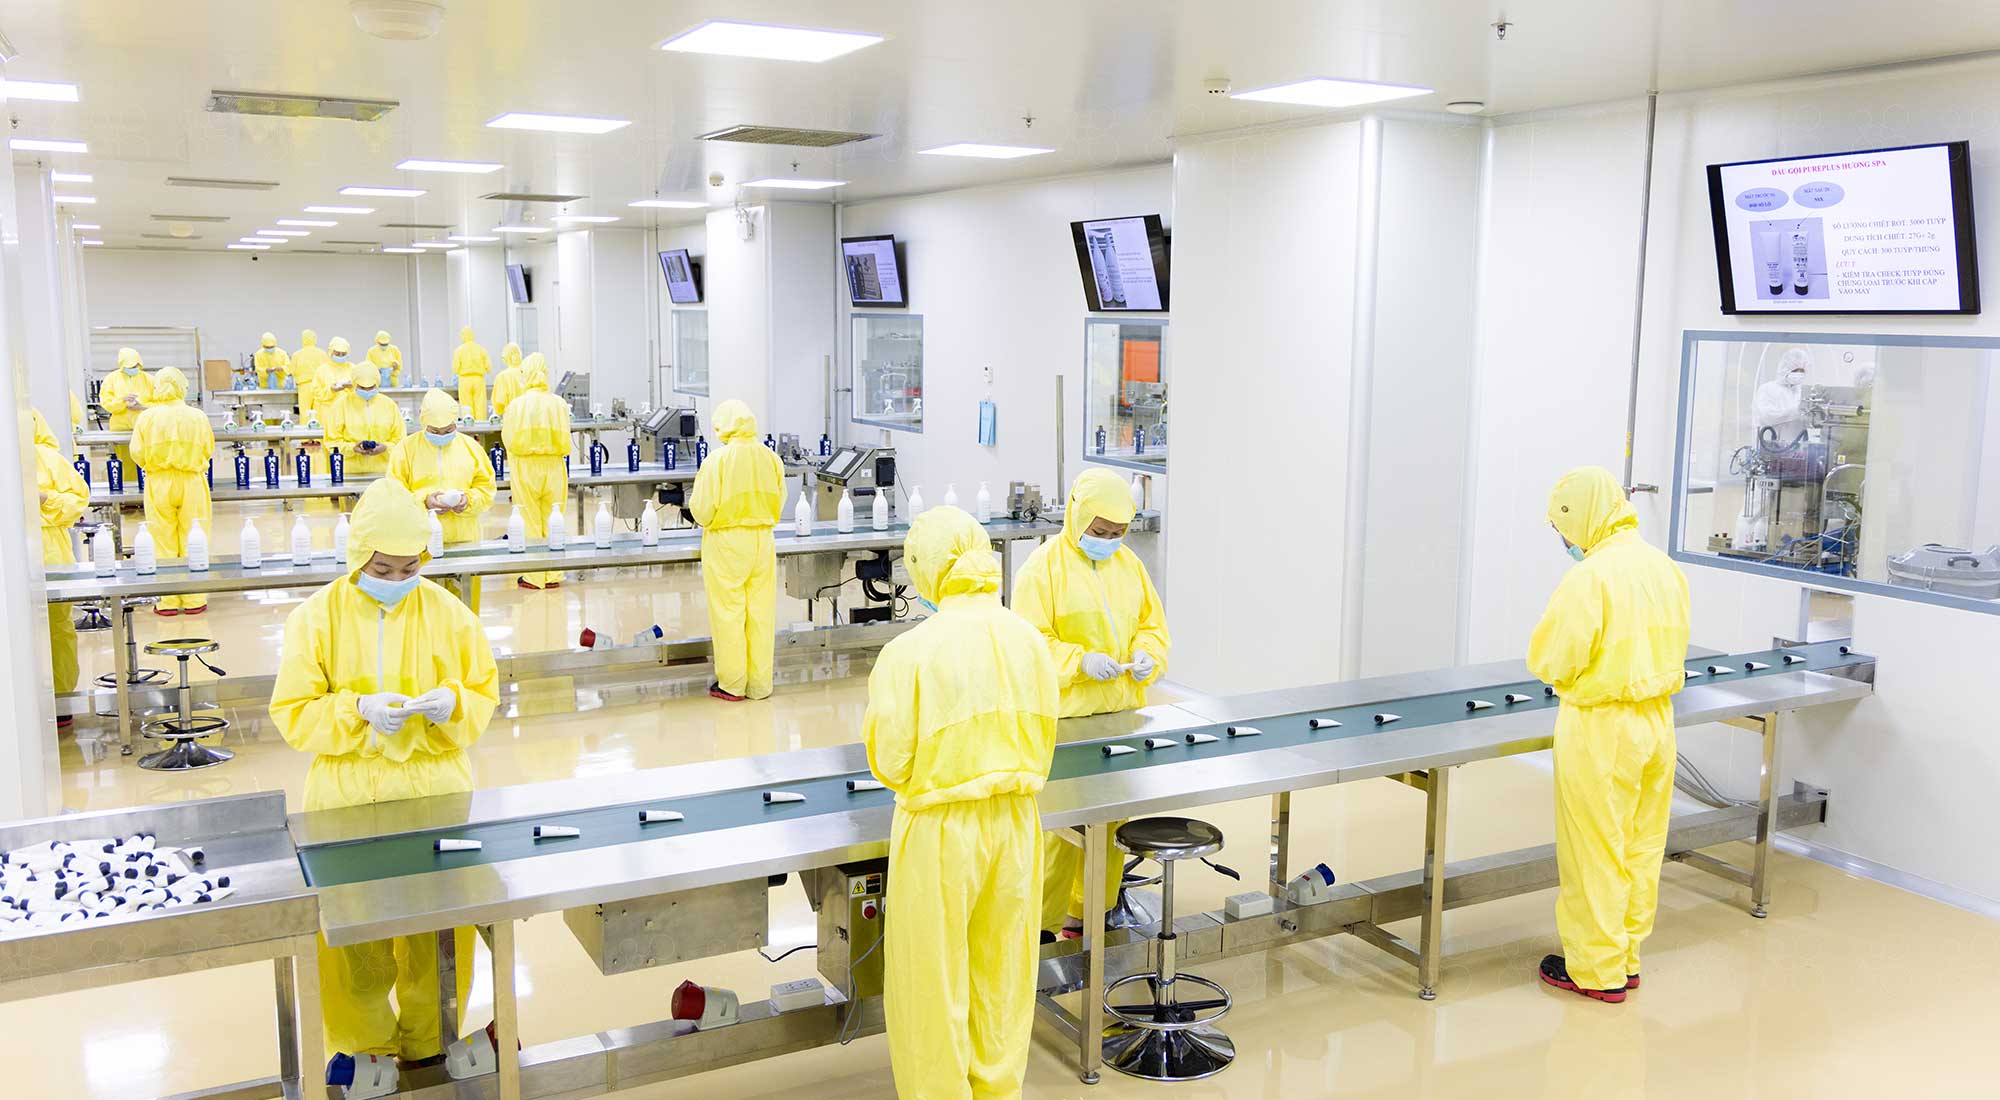
Packaging line
Our filling and packaging operations support a wide variety of container types, including tubes, bottles, and pouches. We can handle both liquids and creams, and offer flexible production for small-lot orders. We also support the manufacturing of small-volume sample products, meeting diverse customer needs.
Inventory Management and Storage
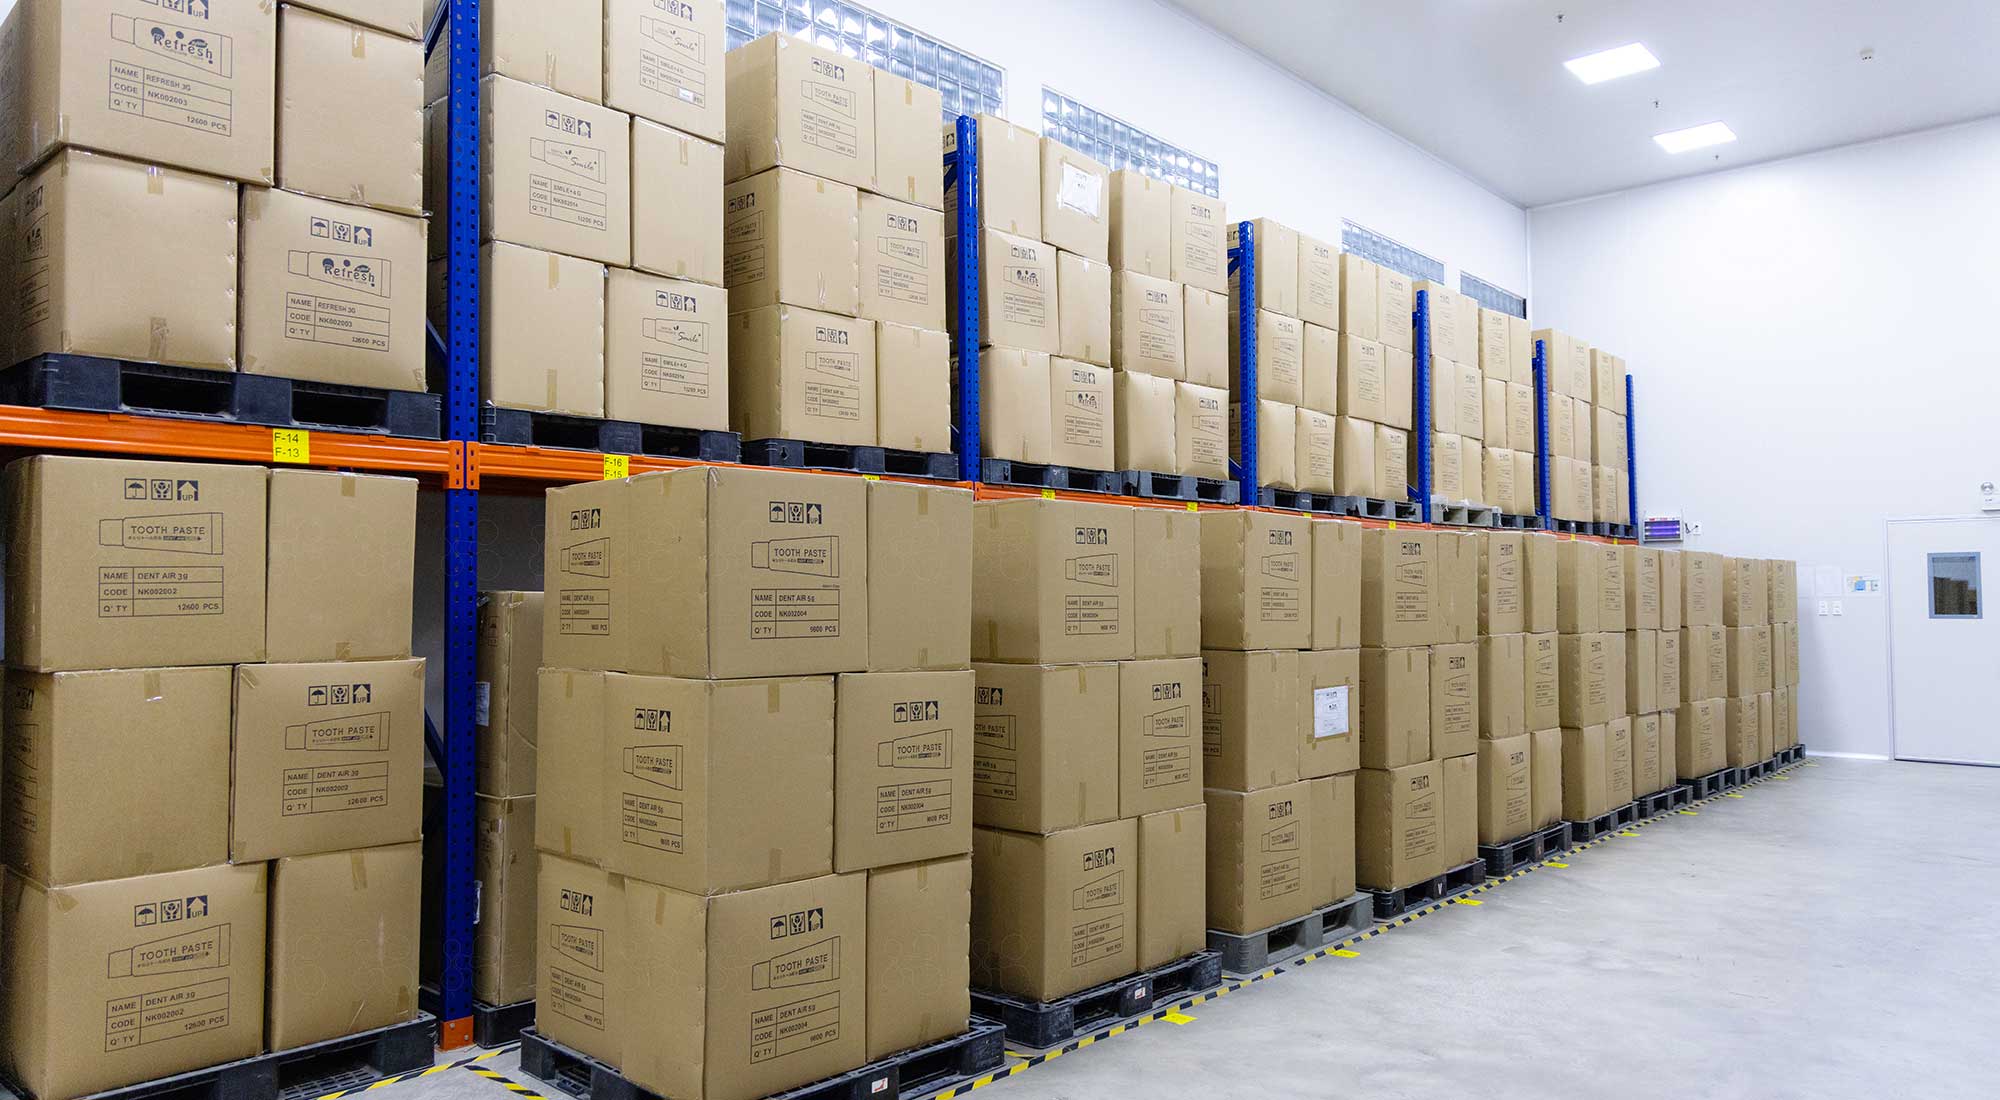
Products and raw materials are properly managed and stored in dedicated warehouses equipped with organized shelving and ample storage space.
Air Conditioning and Purified Water System
In a cGMP-compliant manufacturing facility, the quality of air conditioning and purified water systems is critically important. At our factory, we utilize highly reliable Japanese equipment to deliver clean air and high-purity water stably to the production areas. All systems are subject to regular inspection and maintenance to ensure optimal performance at all times. Few OEM/ODM factories, even internationally, are equipped with systems of this level.
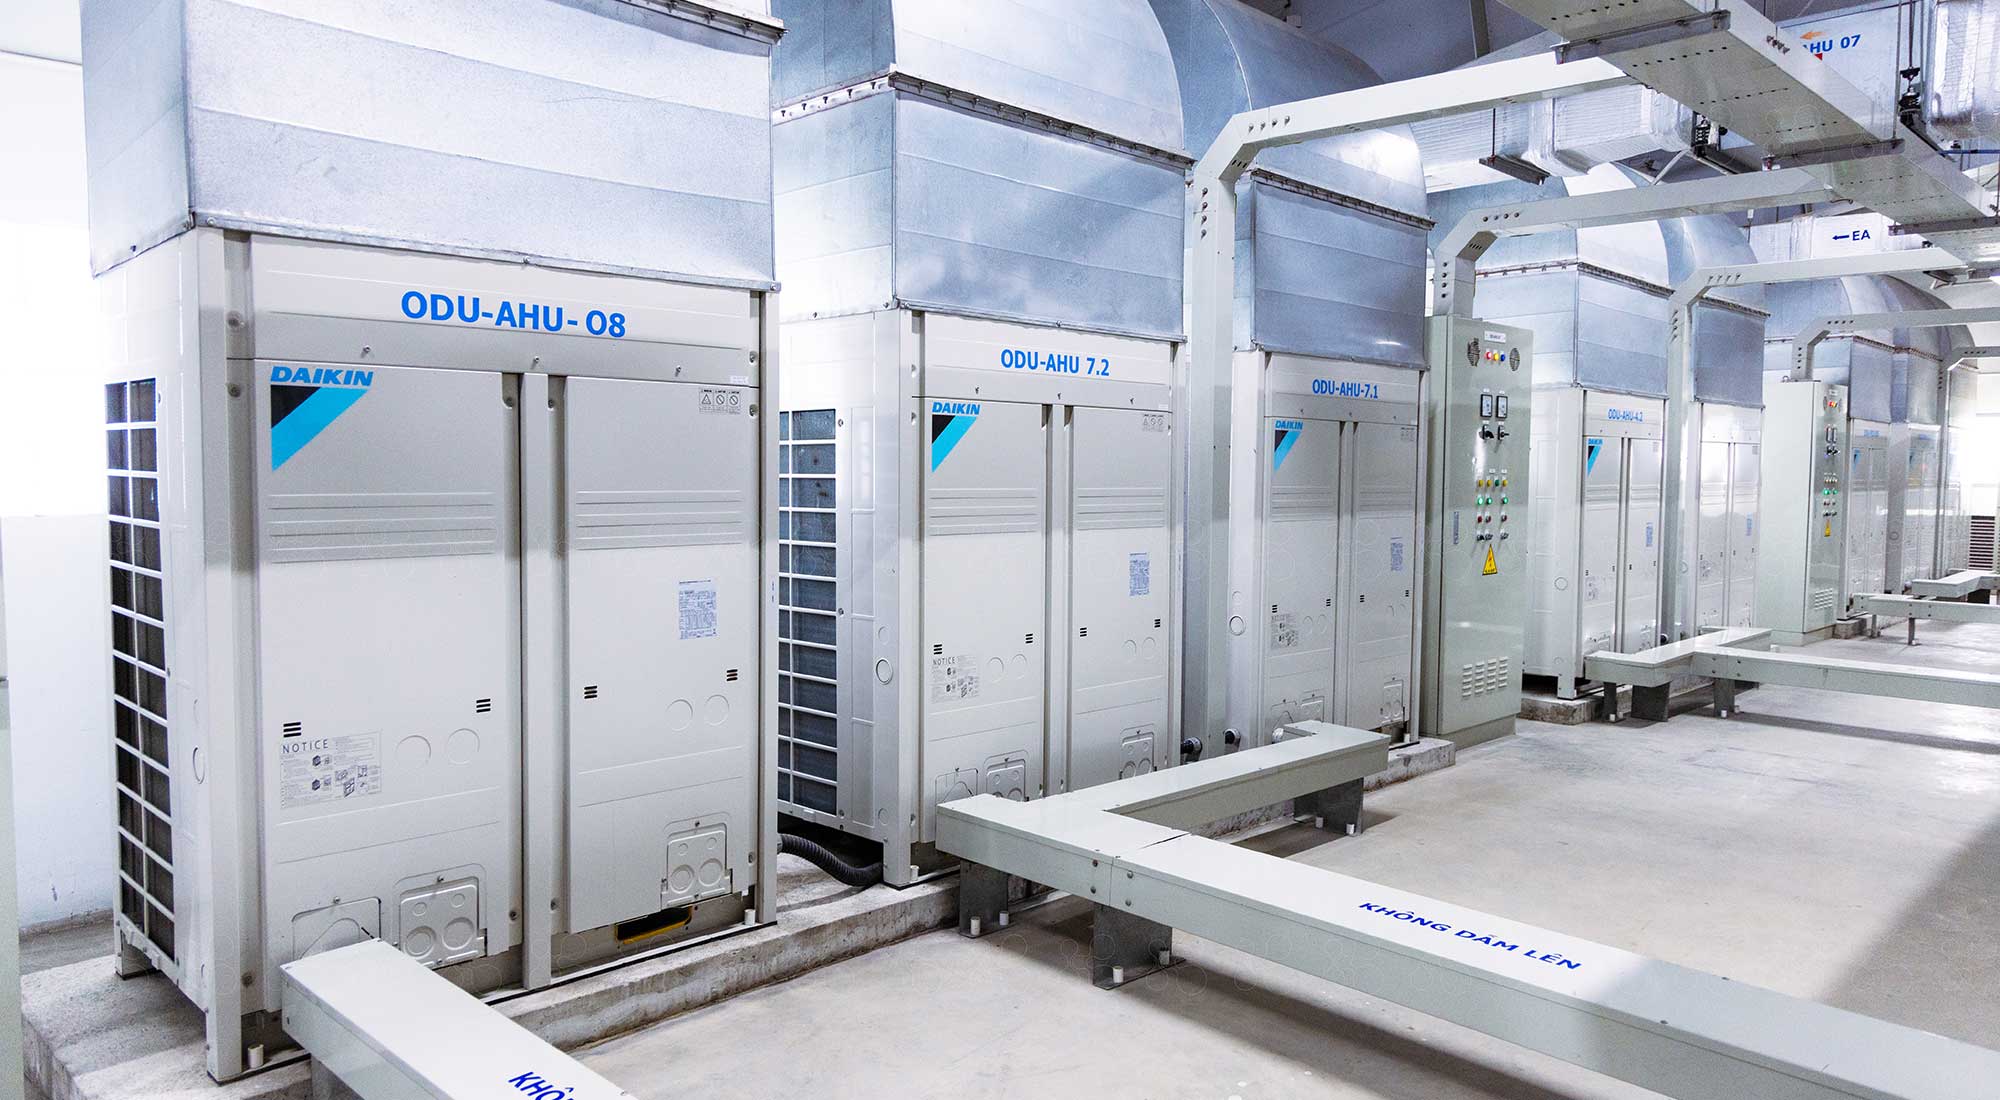
Air Conditioning System
We employ a Daikin air conditioning system that supplies clean air to production areas through HEPA filters. The circulated air is efficiently reused to reduce environmental impact, and positive pressure control is implemented in designated rooms to prevent outside air contamination.
Purified Water System
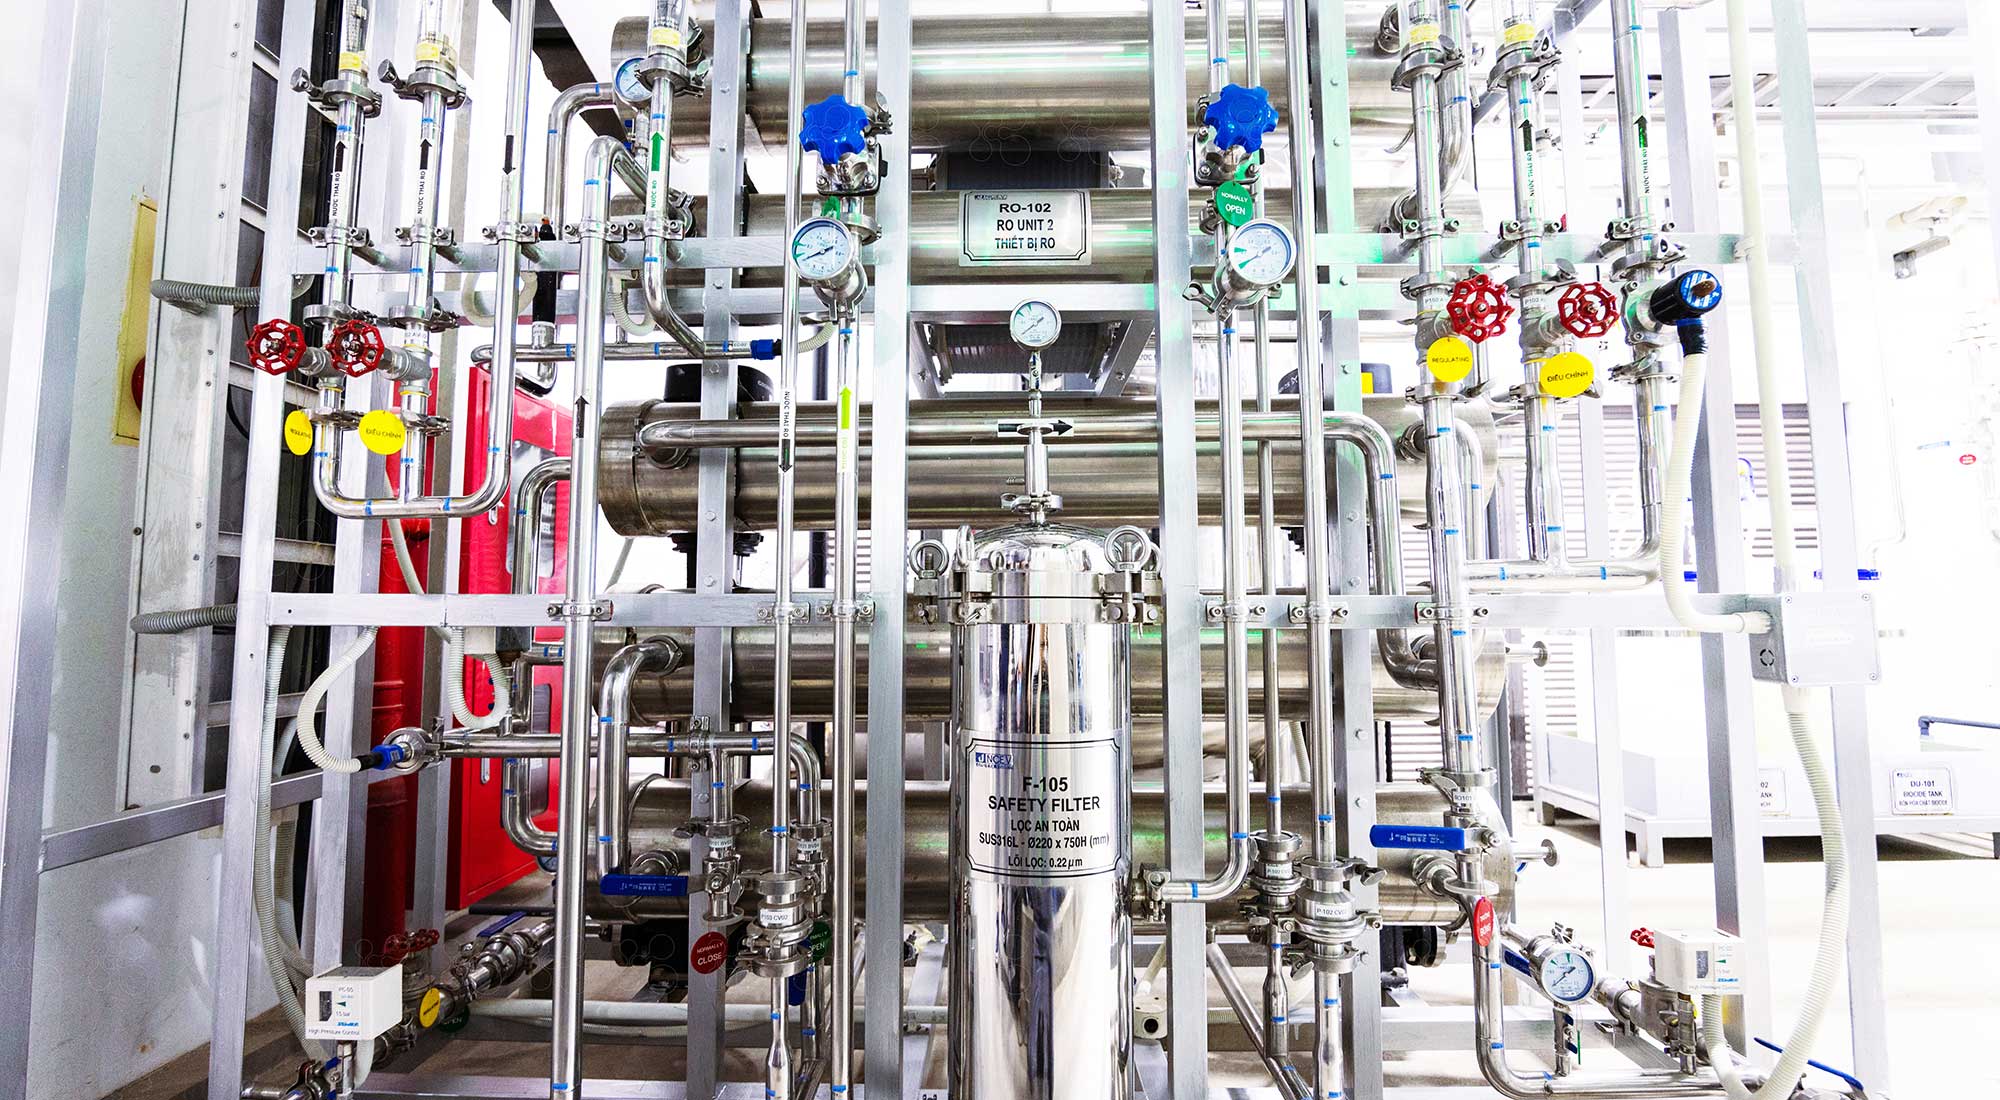
Purified water is produced by processing softened water through sand filtration, activated carbon filtration, and RO units, followed by advanced CDI units. After UV sterilization, the water is supplied to each point of use. Pipes and equipment are regularly sterilized with hot water via heat exchangers to maintain strict hygiene standards.
Hygiene Management
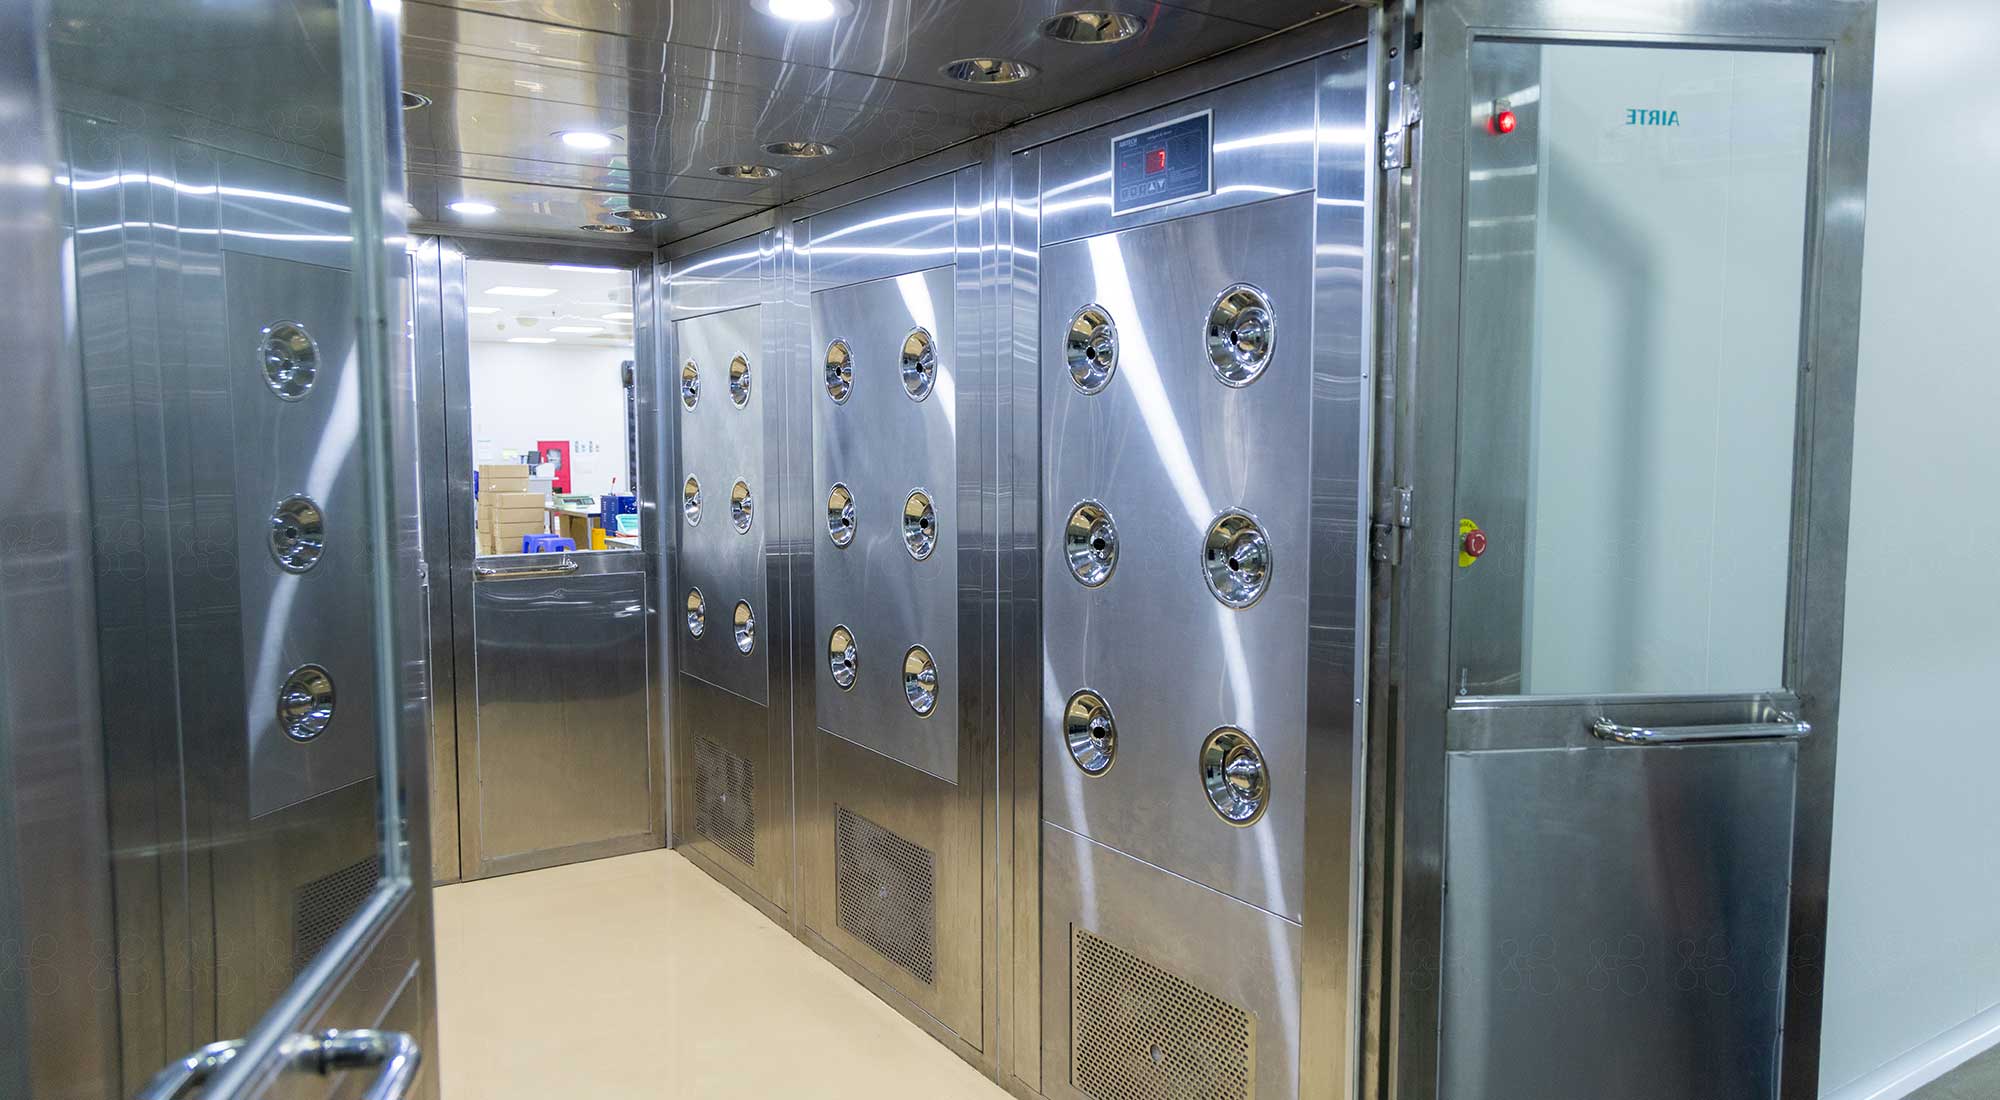
These hygiene protocols ensure that the cleanliness of the production areas is consistently maintained.